Dry Resin Isn’t Necessarily Properly Dried Resin
Most plastics processors understand that hygroscopic materials need to be dried before processing. But there is an important distinction between putting resin through a dryer and knowing that the resin is properly dried.
Seeing the correct temperature and dew point on the dryer display can provide confidence-but it doesn’t tell the whole story.
Proper Drying Requires Four Fundamentals
According to Conair, successful drying of hygroscopic resin depends on four fundamental conditions working together: temperature, time, airflow and dew point.
The resin must reach the correct drying temperature and remain there for the required amount of time. There must also be sufficient airflow through the material bed to transfer heat evenly and carry released moisture away. Finally, the drying air must have a sufficiently low dew point to create the conditions necessary for moisture to migrate out of the pellets.
If any one of these conditions is compromised, the material may not reach the moisture level required for consistent processing.
A Good Dew Point Doesn’t Guarantee Good Resin
Dew point is important, but it measures the condition of the drying air—not directly the moisture content of the resin.
Consider a dryer displaying an acceptable dew point while airflow is restricted by a dirty filter, the hopper is undersized for the required residence time, or material is moving through the system faster than expected.
The dryer may appear to be operating correctly while the resin entering the machine is still above its recommended moisture specification.
That’s an important distinction.
What Happens When Moisture Reaches the Machine?
For hygroscopic materials such as nylon, polycarbonate, ABS and other engineering resins, inadequate drying can contribute to problems including splay, bubbles, brittleness and other cosmetic or mechanical defects. Moisture can also contribute to polymer degradation during processing, meaning the problem isn’t always visible on the surface of the molded part.
The result can be increased scrap, inconsistent quality and unnecessary process adjustments.
Don’t Forget What Happens After the Dryer
Proper drying doesn’t end when material leaves the drying hopper.
Once dried, hygroscopic resin can begin absorbing moisture again when exposed to ambient air. Conveying methods, open machine hoppers, material storage and the time between drying and processing can therefore influence the condition of the resin that ultimately reaches the screw.
Protecting properly dried material through the entire journey from the dryer to the machine is part of maintaining a repeatable process.
Measure the Material, Not Just the Dryer
So how do you know whether your resin is actually dry?
Conair makes an important point in its drying troubleshooting guidance: moisture analysis of material sampled as it leaves the hopper or enters the process is the definitive way to determine whether it has been properly dried.
Monitoring dryer temperature, dew point, airflow and residence time tells you whether the drying process is operating correctly. Moisture measurement tells you whether the material meets the required condition.
Drying Is Part of Process Control
Drying shouldn’t be viewed simply as an auxiliary step before injection molding. For moisture-sensitive materials, it is part of the molding process itself.
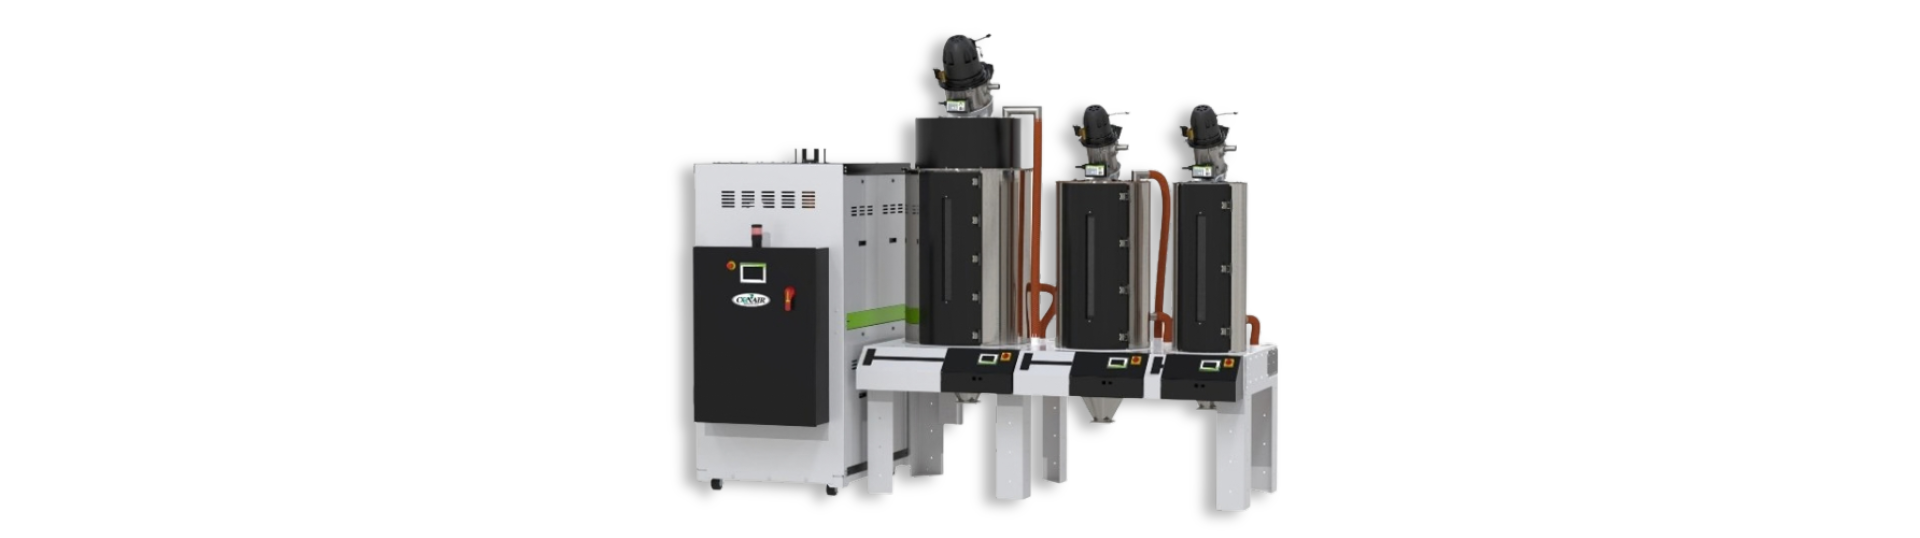
Modern drying systems from Conair provide processors with greater control and visibility over critical drying conditions, helping maintain consistent material preparation while reducing the risk of moisture-related scrap and quality problems.
Because ultimately, the question isn’t: “Is the dryer running?”
It’s: “Is the material entering the machine actually at the moisture level the process requires?”
That difference can have a significant impact on process stability, scrap, part quality and ultimately profitability.
Turner Group can help processors evaluate their material drying, conveying and handling systems to identify opportunities for better material preparation, greater process consistency and reduced waste.