From Signals to Data: Why OPC UA Is Changing Injection Molding Interfaces
For decades, connecting peripheral equipment to an injection molding machine relied largely on dedicated electrical interfaces and hardwired I/O. These solutions worked—and still do—but they were primarily designed to answer relatively simple questions:
Ready? Start? Stop? Fault?
Today’s connected molding cell increasingly needs much more.
From Hardwired Signals to Meaningful Data
Traditional interfaces exchange predefined signals between the injection molding machine and peripheral equipment. Adding functionality can require additional wiring, I/O and programming.
OPC UA takes a different approach. Instead of simply exchanging electrical states, equipment can communicate digitally using standardized information models. Depending on the equipment and interface, that can include operating status, temperatures, pressures, setpoints, alarms and other process information.
The difference is significant: we move from exchanging signals to exchanging meaningful data.
EUROMAP 82 – Putting OPC UA to Work
The EUROMAP 82 series provides practical examples of how OPC UA is being applied within injection molding cells. These include:
- EUROMAP 82.1 – Temperature Control Devices
- EUROMAP 82.2 – Hot Runner Devices
- EUROMAP 82.3 – Liquid Silicone Rubber (LSR) Dosing Systems
Instead of each equipment manufacturer developing its own communication method, these standards establish common information models for communication between the injection molding machine and peripheral equipment.
Bringing the Cell into the Machine Control
One of the important benefits is the potential for more centralized operation.
With compatible equipment, peripheral-device information can be made available through the injection molding machine’s control environment. Operators may be able to view status, process values and alarms—and, where supported, manage permitted settings—without continually moving between separate controllers.
Consider a temperature-control unit. A traditional interface might tell the machine that the TCU is ready or that a fault exists. With standardized OPC UA communication, considerably more information can potentially become available.
The operator can understand not only that something happened, but what is happening.
One Connection to the Production Cell
There is another potentially significant benefit: simplifying MES data collection.
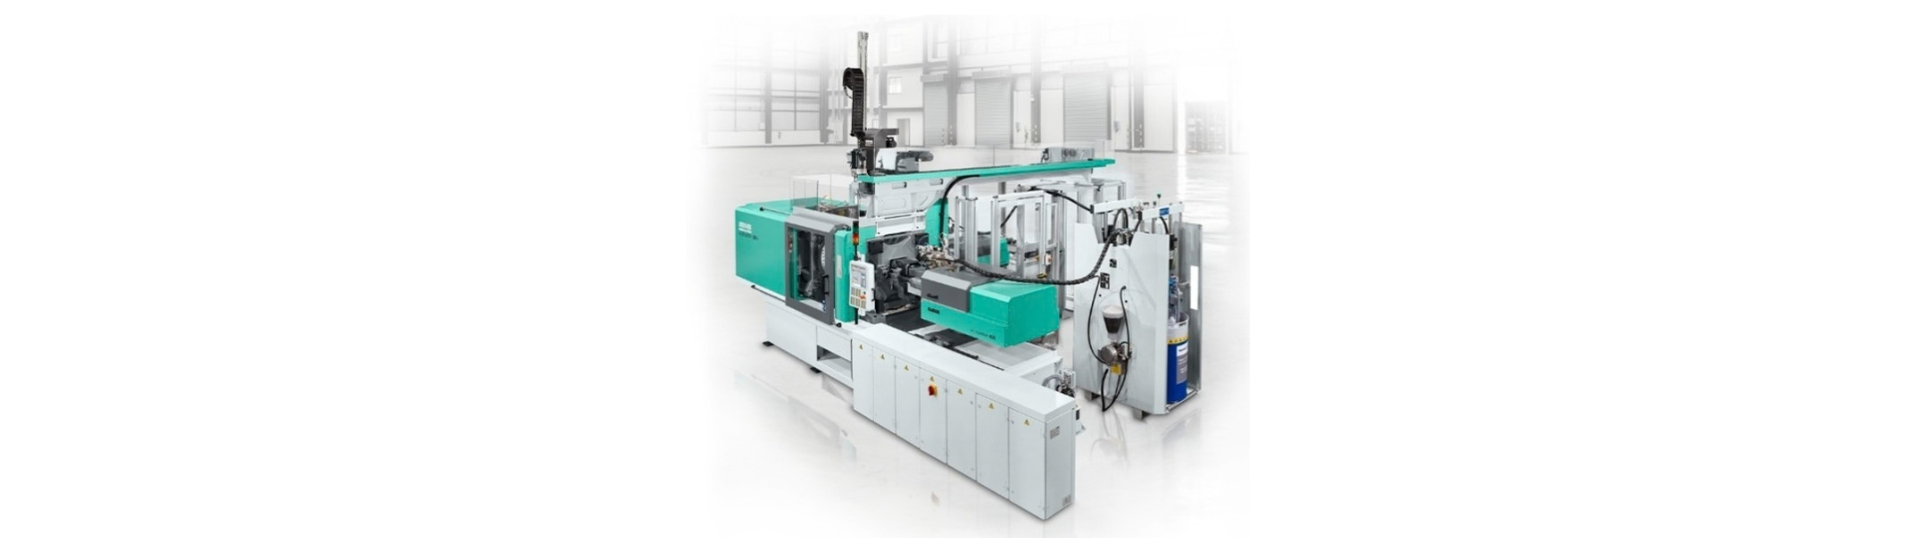
Instead of requiring separate MES connections to every temperature-control unit, hot-runner controller, dosing system or other peripheral, relevant data can potentially be consolidated through the injection molding machine and made available to the higher-level production system.
The architecture can increasingly look like:
Peripheral Equipment → OPC UA / EUROMAP → Injection Molding Machine → MES
The injection molding machine effectively becomes a central data hub for the production cell, giving the MES access to machine information together with relevant data from connected peripherals.
The exact level of integration depends on what the machine, peripheral equipment and applicable interfaces support, but the direction is clear.
Connecting the Complete Molding Cell
Hardwired interfaces aren’t disappearing. For basic machine-to-device functions, they remain proven and effective.
But modern manufacturing increasingly expects more than “Are you ready?”
It wants to know:
“What are you doing, how are you performing, and is something beginning to change?”
That is where OPC UA and standards such as EUROMAP 82.1, 82.2 and 82.3 become particularly valuable.
OPC UA isn’t simply about replacing wires.
It’s about moving from individual pieces of equipment that are connected to a production cell that can meaningfully communicate, be centrally monitored and provide useful data to the systems above it.
Ready to connect more than just the machine?
Talk with Turner Group about how OPC UA and standardized EUROMAP interfaces can help bring your molding machine, peripheral equipment and production data together.